
Client project – Technical solution
Case Packer for Cosmetic Cartons
Product
Cosmetic cartons
Packaging
Company
The customer’s objective was to automate case packing of cosmetic cream cartons in order to increase productivity, ensure gentle product handling and maintain consistent packaging quality. The automation also aimed to reduce operating costs and improve the overall efficiency of the production line.
Project & solution
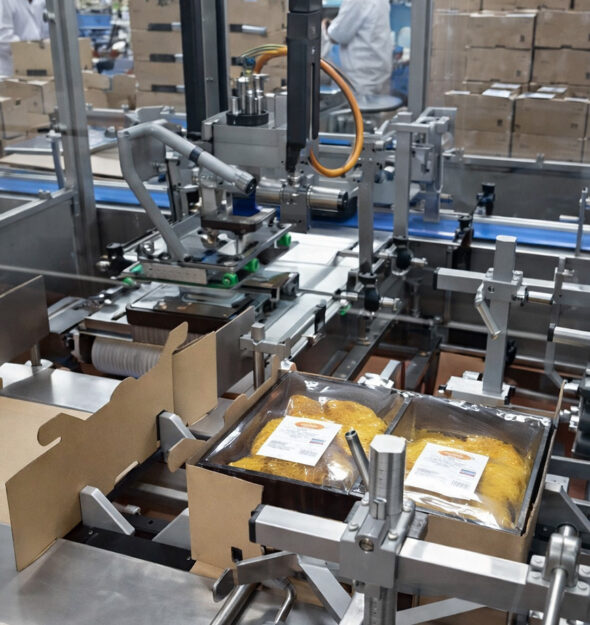
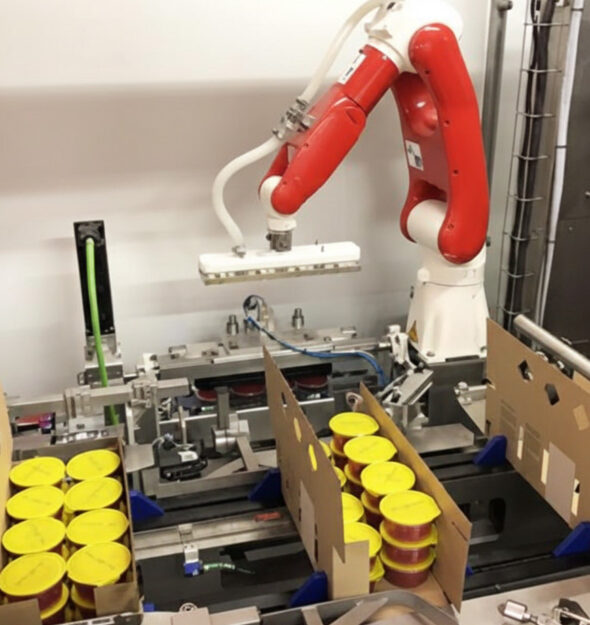
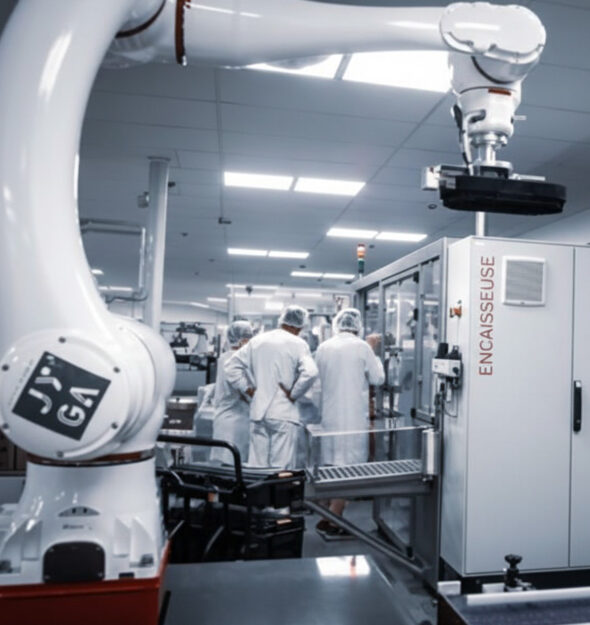
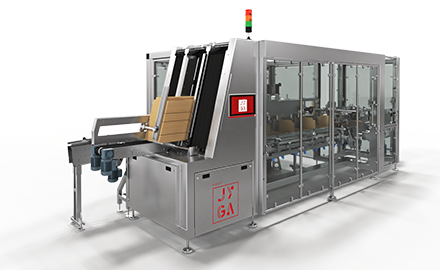
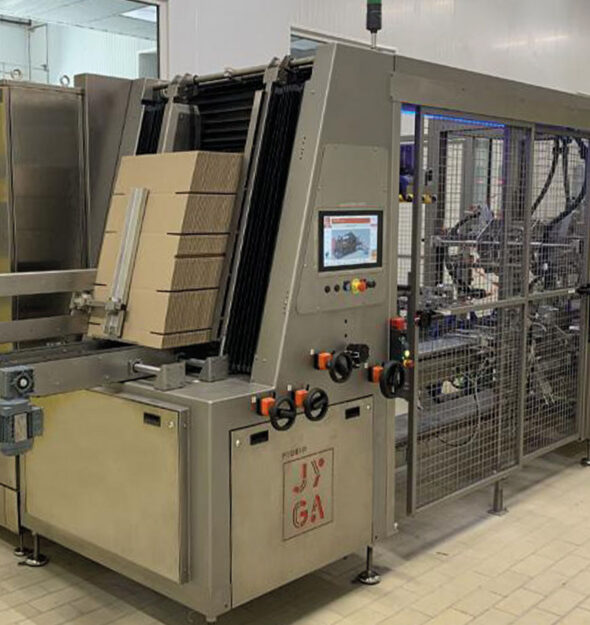
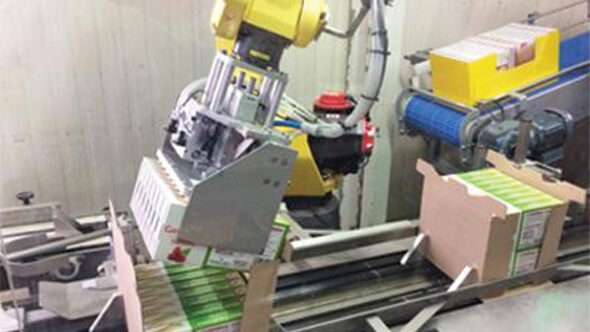
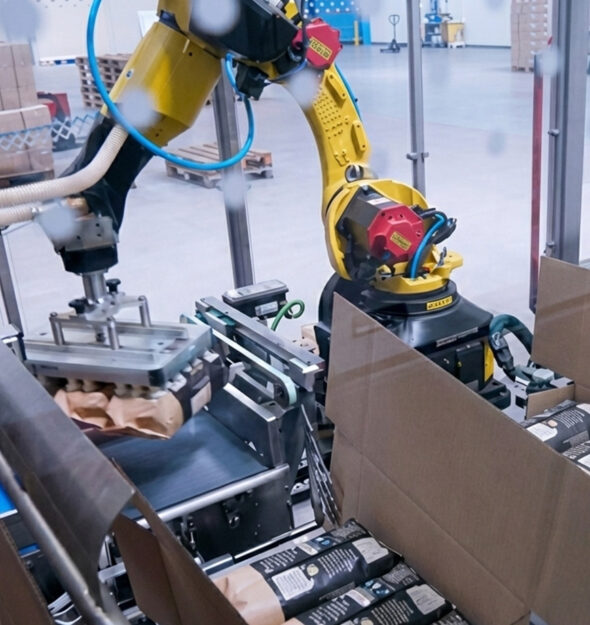
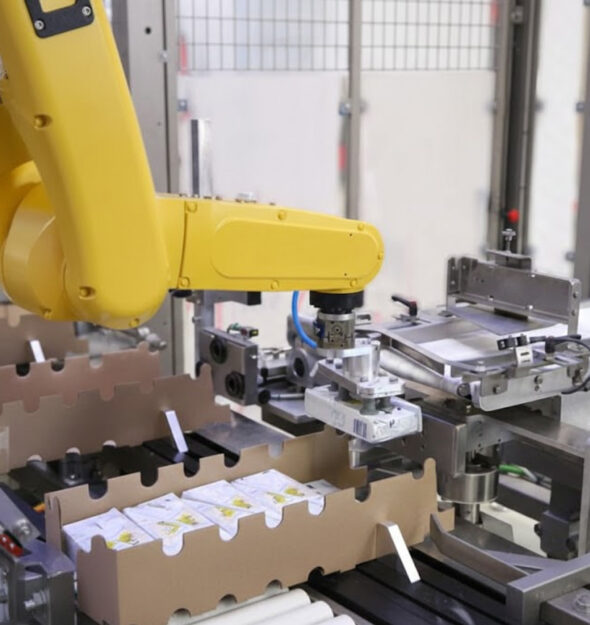
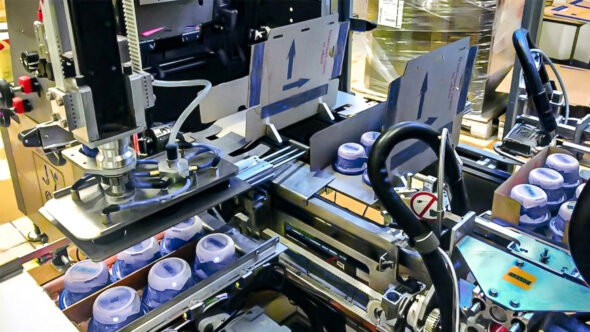
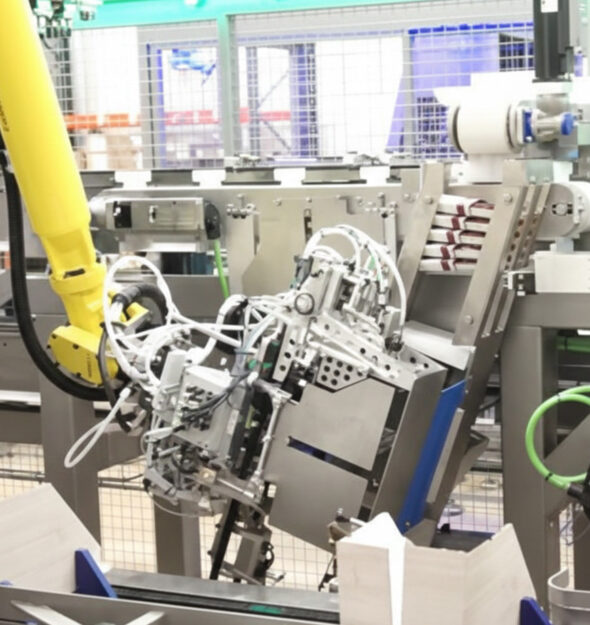
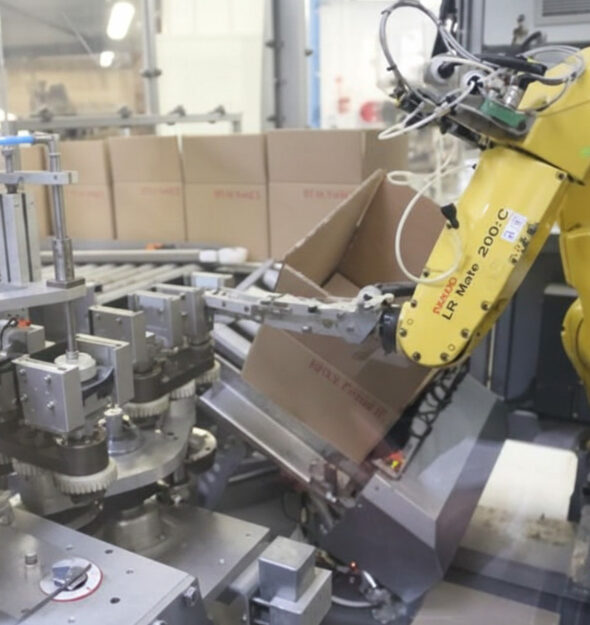
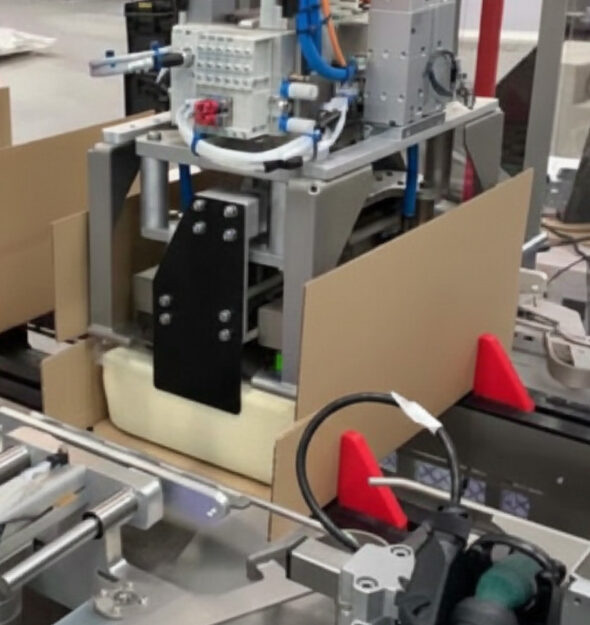
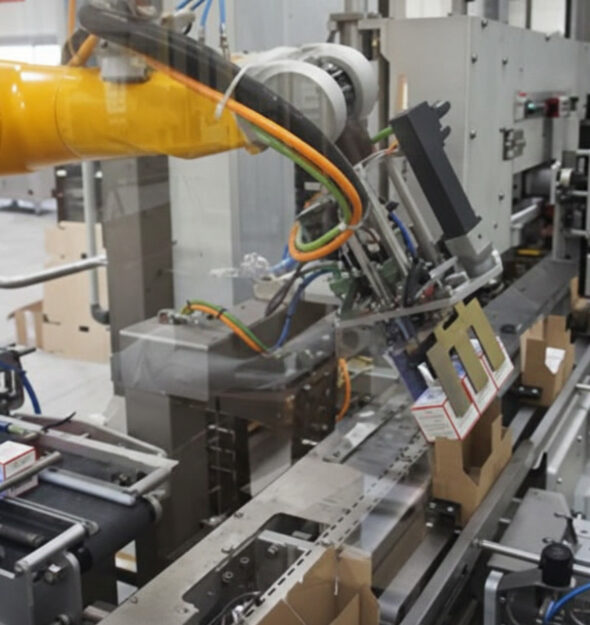
The proposed solution is based on an automatic case packer specifically designed for handling and packing cosmetic cream cartons. The automated machine includes several key functions:
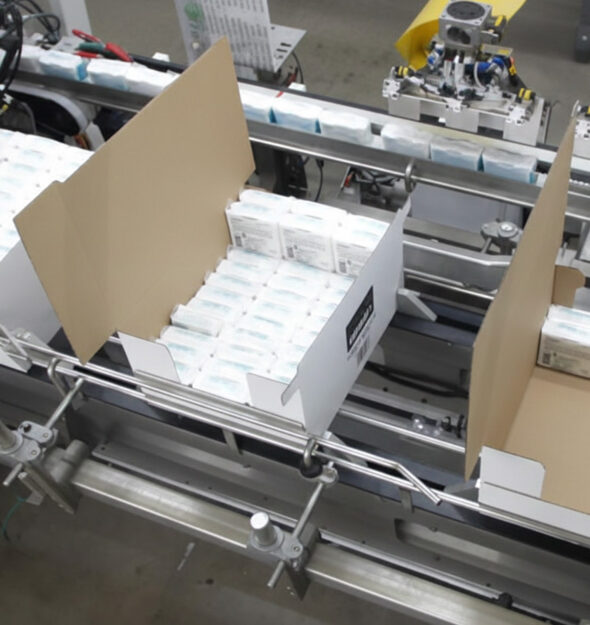
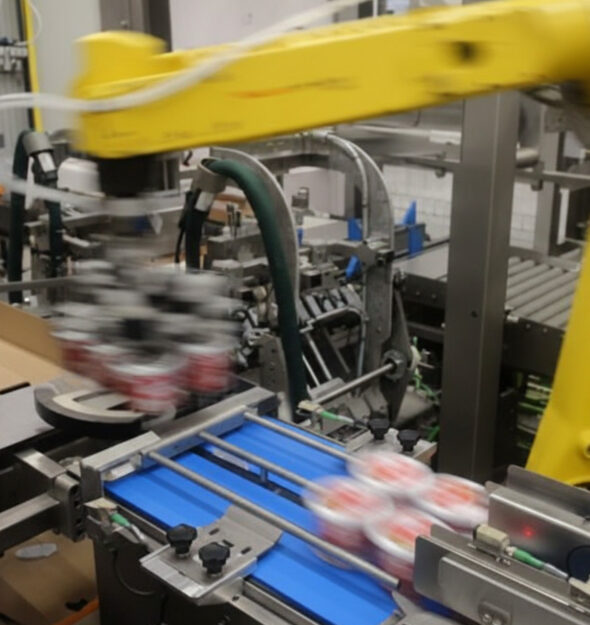
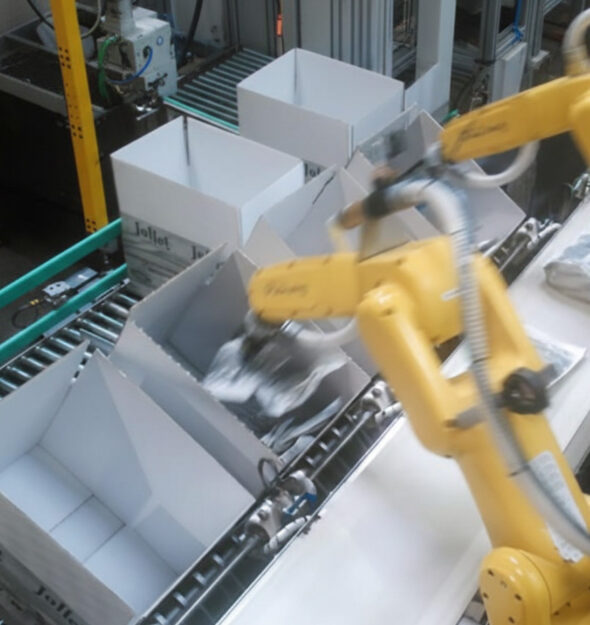
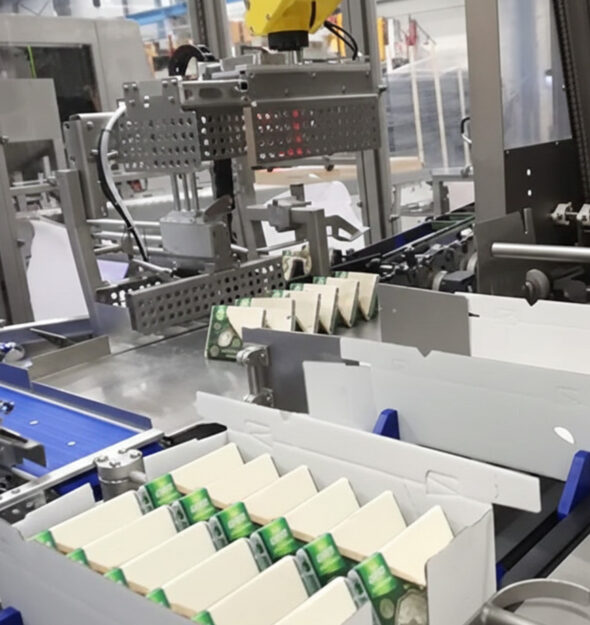
Optimised conveying: a conveyor system guides the cream cartons lying flat to the case-packing area, ensuring smooth, gentle handling.
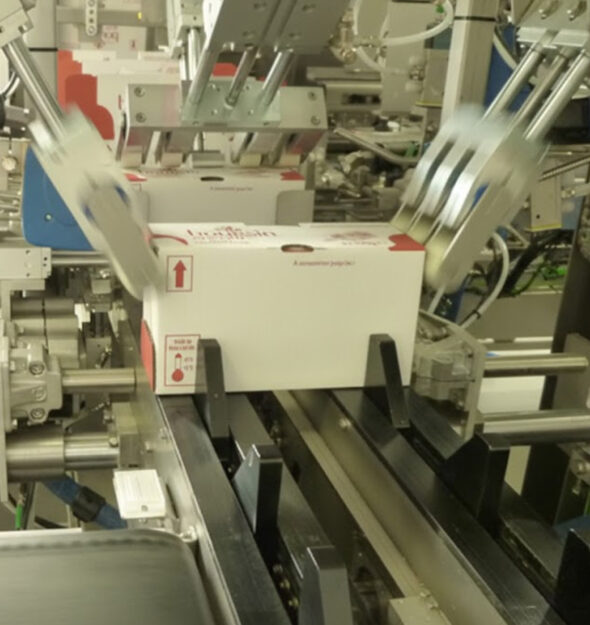
Precise box loading: a synchronised pusher loads the cartons into the boxes accurately and without damaging the products.
High-performance gluing system: a hot-melt glue unit ensures reliable, durable box closing.
Integrated quality control: detection systems including vision sensors and barcode readers verify product and packaging conformity. Non-compliant products are automatically rejected.
Format flexibility: the intuitive HMI enables format changeovers in less than 5 minutes, reducing downtime and increasing efficiency.
Manual bypass: a pass-through option allows manual box loading when required.
Automated labelling: an integrated labeller applies labels correctly and checks them at the outfeed.
By integrating this solution, the customer benefits from a robust, ergonomic and environmentally responsible machine compliant with CE requirements. Appropriate training is provided to ensure rapid adoption by operators and maintenance teams.
Related machine
Side-Load Case Packer
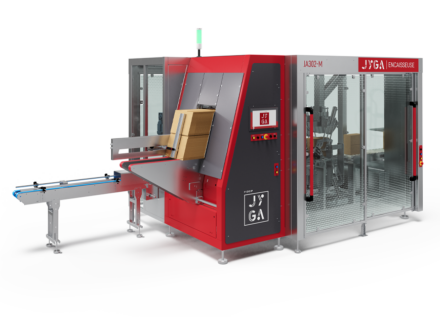
Industrial equipment included in the installation
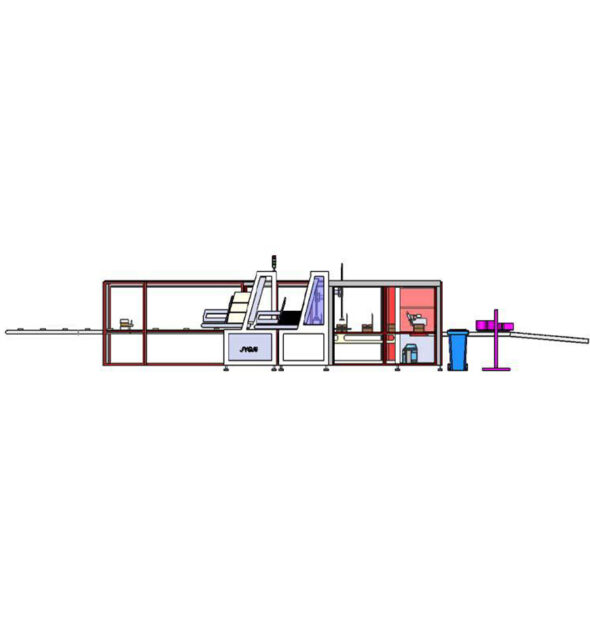
1. Case packer:
- Welded steel frame: painted steel structure providing strength and stability.
- Multi-stage conveyors: manage the arrival of cartons lying flat, loading into boxes and discharge of full boxes.
- Automatic pusher: transfers batches of cartons accurately into the boxes.
2. Gluing system
- High-performance glue unit for strong, reliable box closing.
- Precise adhesive application to minimise consumable waste.
3. Integrated labeller
- Automatic application of labels to the side of the boxes.
- Barcode-reader verification to ensure label conformity.
4. Quality-control system
- Vision sensors to detect packaging defects.
- Automatic discharge of non-compliant boxes to a gravity roller table.
5. Human-machine interface (HMI)
- 15-inch touchscreen with intuitive navigation.
- Diagnostic and format-configuration options directly accessible from the interface.
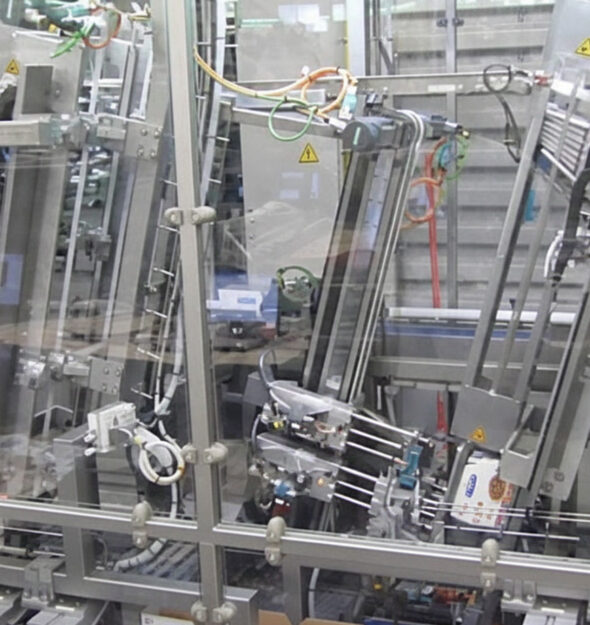
6. Integrated safety system
- Electrically interlocked glass doors to prevent unauthorised access.
- Hard-wired emergency stops for immediate machine shutdown.
Benefits of the JYGA solution
- Proven reliability: JYGA automatic case packers are used by many manufacturers in the cosmetics and personal-care industries.
- Greater flexibility: accommodates a wide range of formats with simplified adjustments.
- Easier maintenance: quick component access and accurate diagnostics via the HMI.
- Environmental commitment: eco-conscious design combined with offsetting initiatives such as tree planting.
Our latest case studies in case packing
Would you like similar equipment?
We are here to advise you and propose solutions tailored to your needs